
The Economic Landscape: The Costly Threat of TiO2 Adulteration
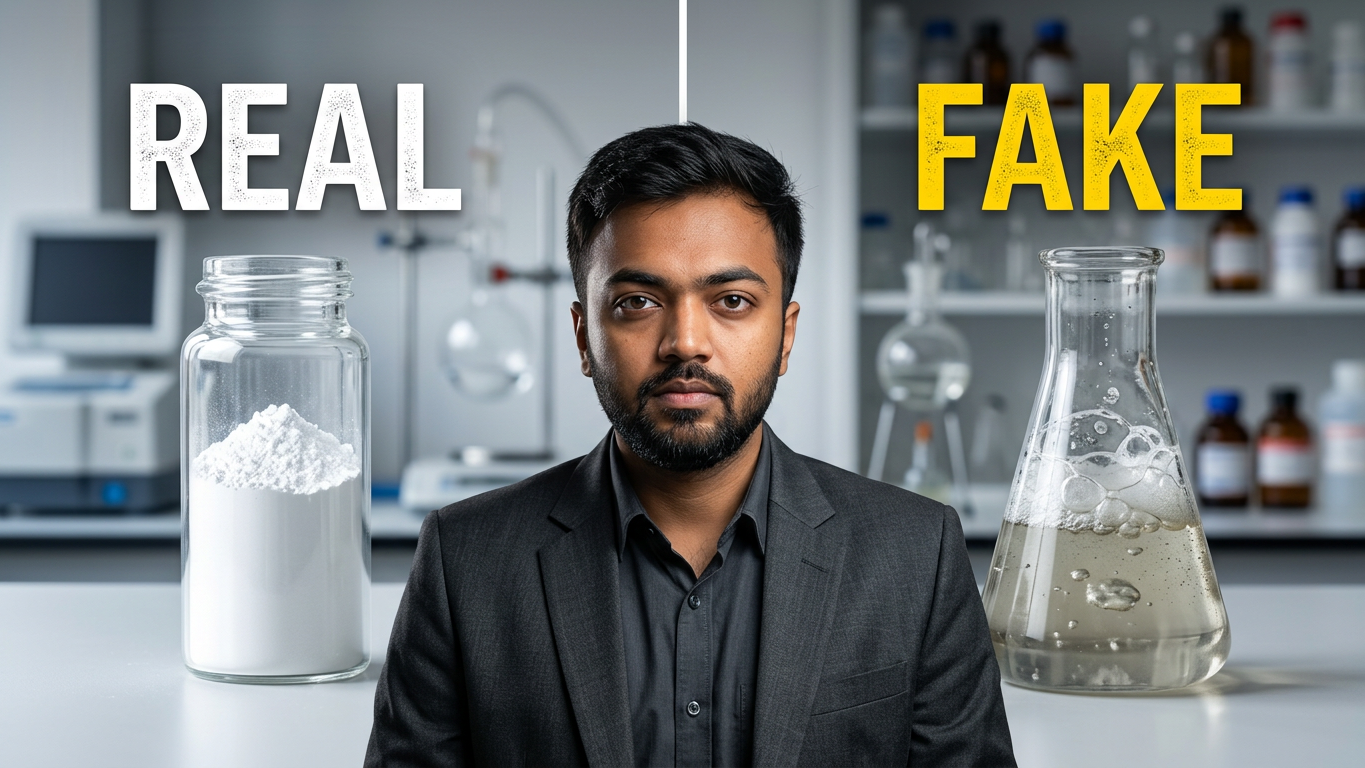
In the paint and coatings industry, titanium dioxide (TiO2) is the “white gold” that dictates a product’s technical and commercial viability. In a market where margins are already thin, verifying the purity of incoming TiO2 isn’t a technical formality – it’s a direct defense of a company’s capital. The incentive for fraud comes down to a stark price gap: pure Rutile TiO2 commands roughly Rs 250–280/kg, while common adulterants like calcium carbonate cost only Rs 10–12/kg, and barium sulfate – now around Rs 60/kg, up sharply from its earlier Rs 30–35/kg range – offers unscrupulous suppliers a lucrative margin.
This pressure has produced a well-established pattern of 20% to 25% substitution. Beyond simple inert fillers, there’s a subtler trap: Anatase TiO2 being used to pass total-purity tests, since it technically is TiO2. But because Anatase lacks the UV resistance and weatherability of Rutile, it inevitably fails in high-performance applications – and the supplier’s savings become the manufacturer’s liability the moment the finished paint film starts to fail.
Performance Degradation: The High Price of Low Quality
The true cost of adulteration rarely shows up on a ledger – it shows up in the failure of the paint film and the slow erosion of brand equity. For smaller manufacturers especially, these failures often manifest as an invisible loss of market share, where repeat orders quietly dry up because the product simply didn’t perform as promised.
Three technical KPIs take the hit: specular gloss, since fillers like calcium carbonate disrupt the refractive index and surface smoothness; opacity or hiding power, since any TiO2 substitution forces the end-user to apply more coats to achieve the desired hide, raising application costs; and film integrity, since substitution alters the pigment volume concentration (PVC) balance and leads to chalking and premature film breakdown. Proactive incoming quality assurance (IQA) is the first and best line of defense against all three.
Incoming QA: Detection Protocols Before Production
Testing raw materials the moment they’re unloaded is the only way to prevent contaminating an entire production batch, and the fastest checks require almost no investment.
The acid fizz test catches calcium carbonate, the most common low-cost filler. Pure TiO2 is chemically inert, so place a small sample in a glass beaker and add a few drops of dilute hydrochloric acid: effervescence or bubbling is a positive indicator of CO2 release from calcium carbonate, while pure TiO2 stays completely inert.
The specific gravity test catches barium sulfate, which is difficult to spot visually but has a distinct physical profile. Using a density cup or pycnometer, Rutile TiO2 should register a specific gravity of 4.0–4.2 as stated on the Certificate of Analysis (COA); barium sulfate reads significantly higher, around 4.5, so any consistent reading well above the COA figure is a clear indicator of barium weighting.
Post-Production Lab Diagnostics: Advanced Verification Methods
Secondary verification confirms the material behaves as TiO2 should once it’s in a formulation. Seven diagnostic protocols are worth running as a matter of routine: checking the oil absorption value against the grade’s TDS figure, since any deviation points to a foreign filler; a tint strength test, mixing a 5% TiO2 sample with 95% pigment (carbon black or alpha blue) in a standard resin system, where a lighter tone confirms high TiO2 content and a darker tone reveals insufficient TiO2; an acid-wash weight reduction test to quantify dissolved calcium carbonate; elemental analysis using a handheld XRF gun for exact percentages of titanium, barium, and calcium; a hiding power drawdown comparison against a known standard; comparative gloss testing on dried films; and a UV stability or chalking test, which is essential for catching the Anatase trap by confirming the film holds up to accelerated weathering at Rutile-level durability.
Forensic Packaging Analysis: Identifying Telltale Clues
Observational expertise is often as effective as chemical analysis, since authentic TiO2 follows industrial packaging standards that manual “mixers” struggle to replicate. Genuine factory bags hold a strict weight tolerance of 24.5–25.5 kg, versus inconsistent fills (23, 26, or 27 kg) from manual packers. High-quality plastic inner liners are always present in authentic shipments but often absent – replaced by single-layer paper bags – in adulterated ones. Genuine shipments arrive industrially shrink-wrapped and compressed, while adulterated stock tends to show loose bags with no industrial compression. Documentary evidence matters too: a legitimate COA carries the importer’s name, stamps, and signatures, while a blank importer name or an edited-looking COA is a red flag. Compression itself is a useful tell – authentic containers from major hubs like China are compressed to 24–27 tons for maximum tonnage, while manually packed, uncompressed loads typically max out around 20 tons.
Establishing a Culture of Verification
Protecting a manufacturer’s reputation requires moving beyond simple price-hunting. Catching a sophisticated adulterator is genuinely difficult, but choosing the right supplier and running these verification steps consistently makes it manageable. The final directive is straightforward: check every COA for lot numbers, stamps, and signatures, and be particularly wary of any COA where the importer’s name is blank or appears to have been modified. Quality isn’t a shop-floor suggestion – in an industry built on trust in raw materials, it’s a data-driven mandate.


Leave a comment